Chemometric Hyperspectral Imaging For the Automation World
Hinalea Imaging Corp.'s VNIR CORE system brings a cost-effective solution to the industrial adoption of hyperspectral imaging.
Published October 5, 2026
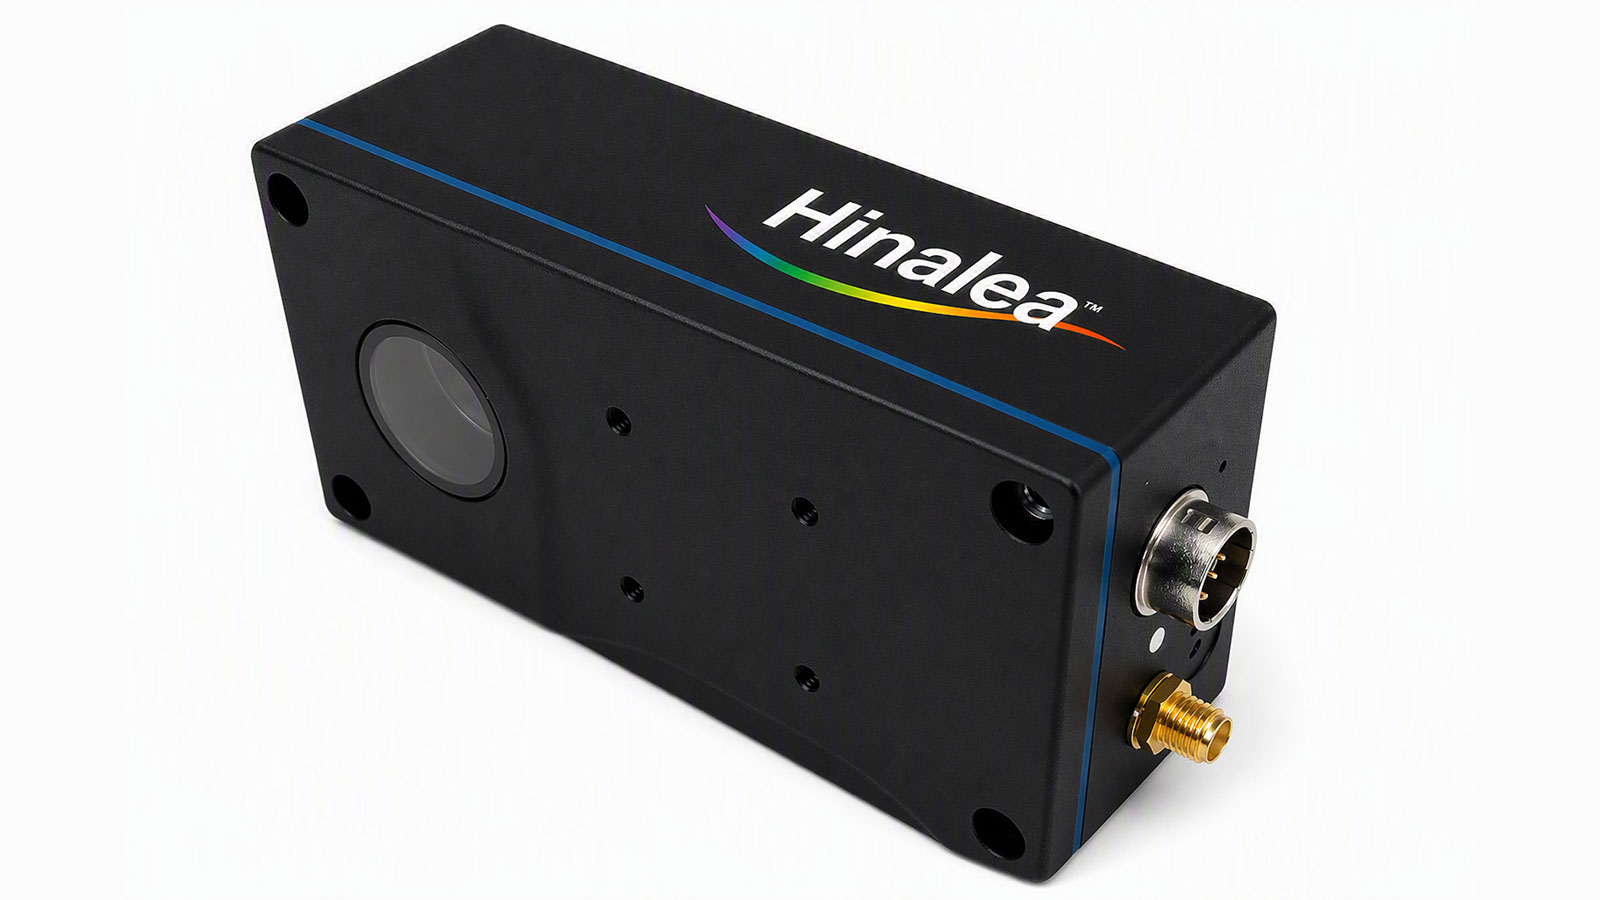
Hinalea Imaging Corp.'s VNIR Core system is designed for industrial applications such as inspection equipment and machine vision systems.
Hinalea Imaging Corp., a provider of intelligent hyperspectral imaging (HSI) solutions, announced the launch of the Hinalea VNIR CORE system, a compact, cost-effective imaging system for the visible and near-infrared (VNIR) spectral range designed to accelerate the industrialization of hyperspectral imaging.
The VNIR CORE system reduces HSI hardware cost by approximately 70% compared to conventional VNIR hyperspectral systems, addressing one of the primary barriers to widespread industrial adoption. Its MEMS-based architecture combines compact form factor, spectral intelligence, and significantly improved economics, enabling hyperspectral imaging to move beyond research laboratories and into high-volume production and inspection environments.
By making advanced spectral sensing substantially more accessible, VNIR CORE enables manufacturers to apply laboratory-grade chemical and material analysis directly within industrial workflows. The platform is designed to support a new generation of intelligent imaging applications capable of detecting chemical composition, material properties, quality attributes, contamination, and defects that conventional machine-vision systems cannot see.
"For years, hyperspectral imaging has largely remained the domain of laboratory research, with the cost and complexity of sensors limiting commercial adoption," said Barry McDonogh, CEO of Hinalea Imaging. "VNIR CORE is the first in a new series of products designed to change that equation. By dramatically reducing hardware cost while retaining the spectral intelligence that makes HSI so powerful, we can bring laboratory-grade chemometrics to industrial inspection and enable hyperspectral imaging to be deployed at scale."
The Hinalea VNIR CORE is being showcased at the upcoming VISION 2026 machine vision trade fair in Stuttgart, Germany, October 6th through 8th.
About the VNIR CORE system: The VNIR CORE covers the 420–980 nm visible and near-infrared spectral range. Measuring just 112 × 56 × 34 mm and weighing 235 grams, it is designed for integration into OEM platforms, machine vision systems, industrial inspection equipment, and drone-based imaging platforms. It delivers 14 nm FWHM spectral resolution across 40 spectral bands, with 1280 × 1024-pixel spatial resolution. USB 3.0 connectivity and 4.5-watt power consumption support deployment in applications where reduced size, weight, and power are important.